


 Send Inquiry
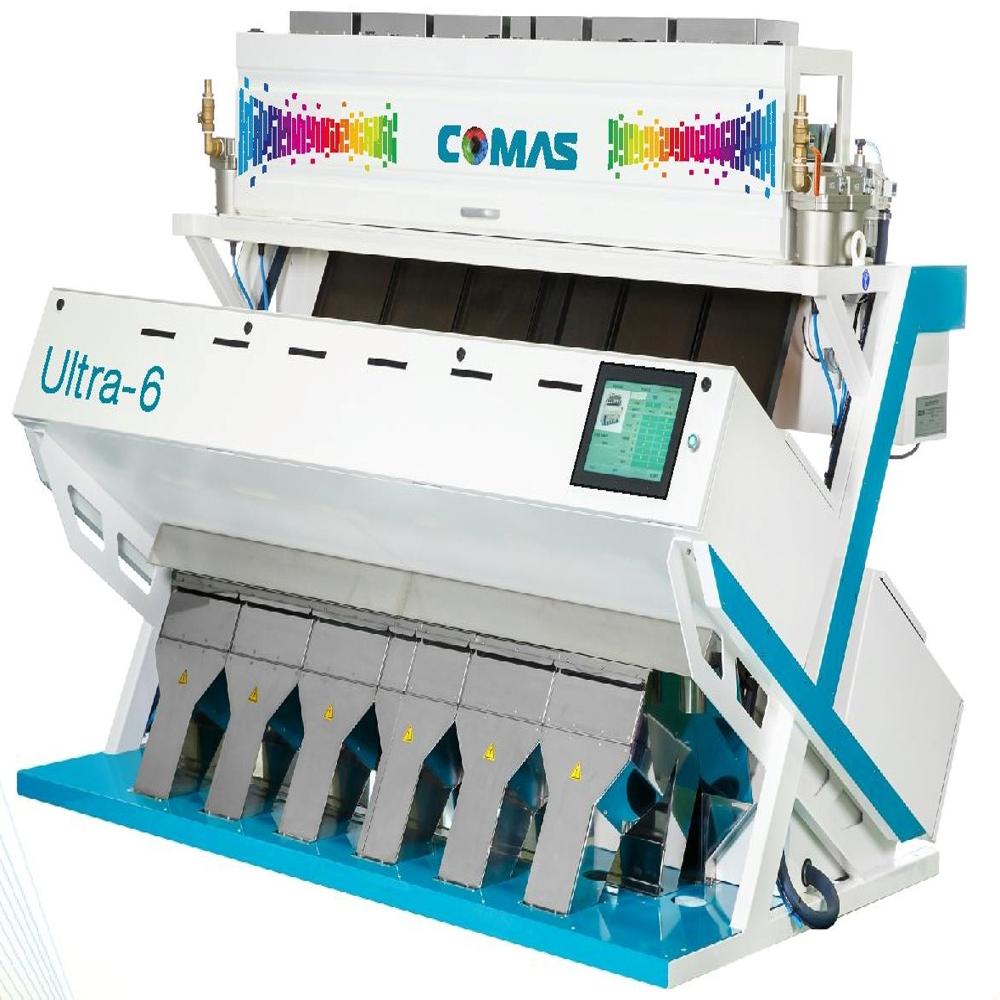
Cashew Nut Color Sorter
Price 500000.0 INR/ Unit
MOQ : 1 Unit
Cashew Nut Color Sorter Specification
- Application
- Sorting Cashew Nuts
- Weight
- 950 kg
- Usage
- Industrial
- Air Compressor
- Required (5.5 kW, 7.5 HP)
- Capacity
- 300-500 Kg/hr
- Power
- 2.5 kW
- Type
- Cashew Nut Color Sorter
- Accuracy
- 99%
- Air Pressure
- 0.6-0.8 MPa
- Dimension (L*W*H)
- 2000 mm x 1620 mm x 1770 mm
- Output
- 3-5 Ton/Day
- Channels
- 64 Channels
- Voltage
- 220V/50Hz
- Operating Temperature
- 5C - 40C
- Ejector Type
- High-Speed Electric Valve
- Reject Ratio
- <5%
- Sensor Technology
- CCD High-Resolution Sensors
- Sorting Stages
- Double or Triple Sorting Available
- Suitable Materials
- Cashew Nuts, Dry Fruits, Seeds
- Light Source
- Long-life LED
- Operation Mode
- Automatic with Touch Screen Interface
Cashew Nut Color Sorter Trade Information
- Minimum Order Quantity
- 1 Unit
- Delivery Time
- 10-15 Days
About Cashew Nut Color Sorter
The RGB Rice Sorter is a semi-automatic sorting machine designed for industrial applications. With multiple channels, this machine is capable of sorting rice based on color, size, and quality. It comes with an air compressor to ensure smooth and efficient operation. The output of this machine is normal, making it suitable for medium to large scale rice processing facilities.
FAQs of RGB Rice Sorter:
Q: What is the application of the RGB Rice Sorter?
A: The RGB Rice Sorter is designed for industrial use.Q: What type of sorting machine is it?
A: It is a semi-automatic sorting machine.Q: Does it have multiple channels?
A: Yes, it comes with multiple channels for sorting.Q: What is the output capacity of the machine?
A: The output of this machine is normal.Q: Does it come with an air compressor?
A: Yes, it comes with an air compressor for efficient operation.Precision Sorting Technology
Utilizing advanced CCD high-resolution sensors and a high-speed electric valve ejector system, this sorter ensures superior accuracy (99%) when segregating cashew nuts, seeds, and dry fruits. The double or triple sorting options enable improved product quality and consistency with minimal rejection rates, making it ideal for commercial processing facilities.
Intuitive Operation and High Capacity
Equipped with a user-friendly touch screen interface and automatic controls, the Cashew Nut Color Sorter streamlines operations for users. It reliably processes up to 500 kg per hour, with daily output capacities of up to 5 tons. The combination of high throughput and efficiency supports rapid scaling in industrial environments.
Robust Construction and Adaptability
Manufactured with durable components and designed for industrial use, this color sorter operates optimally in a range of environments between 5C and 40C. Its compatibility with various dry fruits, seeds, and the ability to perform multi-stage sorting make it a versatile solution for distributors, traders, and suppliers throughout India.
FAQ's of Cashew Nut Color Sorter:
Q: How does the Cashew Nut Color Sorter achieve high accuracy in sorting?
A: The Cashew Nut Color Sorter utilizes CCD high-resolution sensors coupled with high-speed electric valve ejectors to precisely detect and separate defective or discolored nuts. Its double or triple-stage sorting capability further enhances sorting accuracy up to 99% while keeping reject ratios below 5%.Q: What types of materials can be processed by this color sorter?
A: This color sorter is primarily designed for cashew nuts but can also efficiently sort other dry fruits and seeds, making it versatile for use in the food processing industry where consistent quality is critical.Q: When should I use the double or triple sorting feature?
A: Select double or triple sorting stages when a higher level of product purity is desired or when handling batches with significant color variations. These options help achieve stringent quality standards required by demanding markets.Q: Where is this machine typically installed and used?
A: The Cashew Nut Color Sorter is intended for use in industrial and commercial processing facilities, such as factories and packaging plants, across India. It is ideal for distributors, traders, and suppliers who deal with bulk quantities of cashew nuts and dry fruits.Q: What is the process of operating this color sorter?
A: Operation is straightforward: feed cashew nuts into the machine, which automatically scans and separates them using advanced sensors and ejectors. The touch screen interface controls sorting parameters, while an air compressor (5.5 kW, 7.5 HP) provides the necessary air pressure for the ejector system.Q: How does the touch screen interface benefit users during operation?
A: The touch screen interface offers a user-friendly experience by simplifying control of sorting stages, adjusting parameters, monitoring performance, and facilitating quick troubleshooting, which improves overall efficiency and reduces downtime.Q: What are the main benefits of using the Cashew Nut Color Sorter for industrial operations?
A: Key benefits include outstanding sorting accuracy, high throughput (up to 5 tons per day), reduced rejects, adaptability to multiple products, robust construction, and simplified operation, all contributing to improved quality control and increased profitability for large-scale processors.
Tell us about your requirement

Price:
Quantity
Select Unit
- 50
- 100
- 200
- 250
- 500
- 1000+
Additional detail
Mobile number
Email

More Products in Sorter Machine Category
Rice Color Sorter Machine
Price 500000.0 INR / Unit
Minimum Order Quantity : 1 Unit
Dimension (L*W*H) : 1470 x 1620 x 1970 mm
Air Pressure : 0.60.8 MPa
Accuracy : 99%
Channels : 64

Pulses Color Sorter
Price 500000.0 INR / Unit
Minimum Order Quantity : 1 Unit
Dimension (L*W*H) : 2100 x 1630 x 2040 mm
Air Pressure : 0.8 MPa
Accuracy : 9899%
Channels : 192

Groundnut Sorter Machine
Price 500000.0 INR / Unit
Minimum Order Quantity : 1 Unit
Dimension (L*W*H) : 2160 x 1560 x 1750 mm
Air Pressure : 0.6 0.8 MPa
Accuracy : 99%
Channels : 64 Channels

Wheat Sorting Machine
Price 500000.0 INR / Unit
Minimum Order Quantity : 1 Unit
Dimension (L*W*H) : 2100 1590 1895 mm
Air Pressure : 0.60.8 MPa
Accuracy : 99%
Channels : 63

GST : 36ABICS0252L1Z6
Plot No 63, Hi-tech Theater Ln, Arunodaya
Colony, Sri Sai Nagar, Madhapur,Hyderabad - 500081, Telangana, India
Phone :07971671060
 Send Inquiry
|
 |
SAANVIKA SOFTWARE SOLUTIONS PRIVATE LIMITED
All Rights Reserved.(Terms of Use) Developed and Managed by Infocom Network Private Limited. |
