


 Send Inquiry
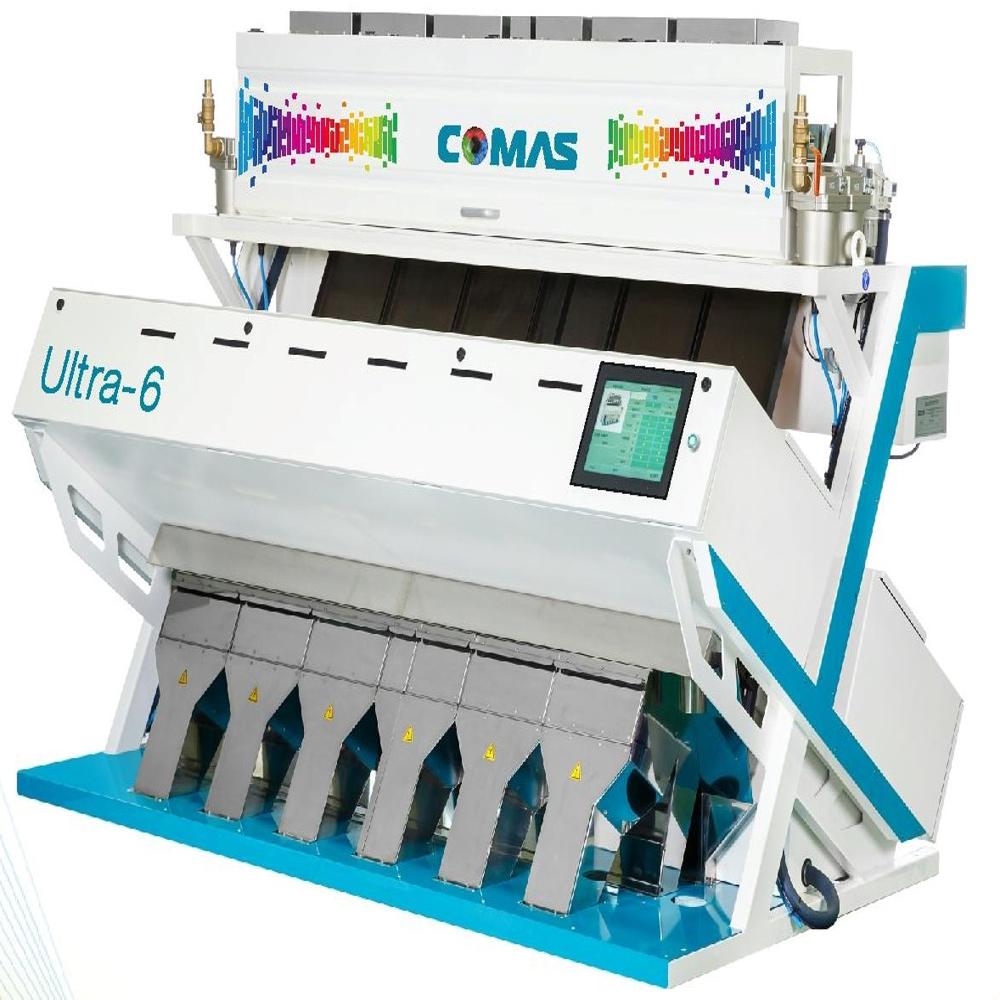
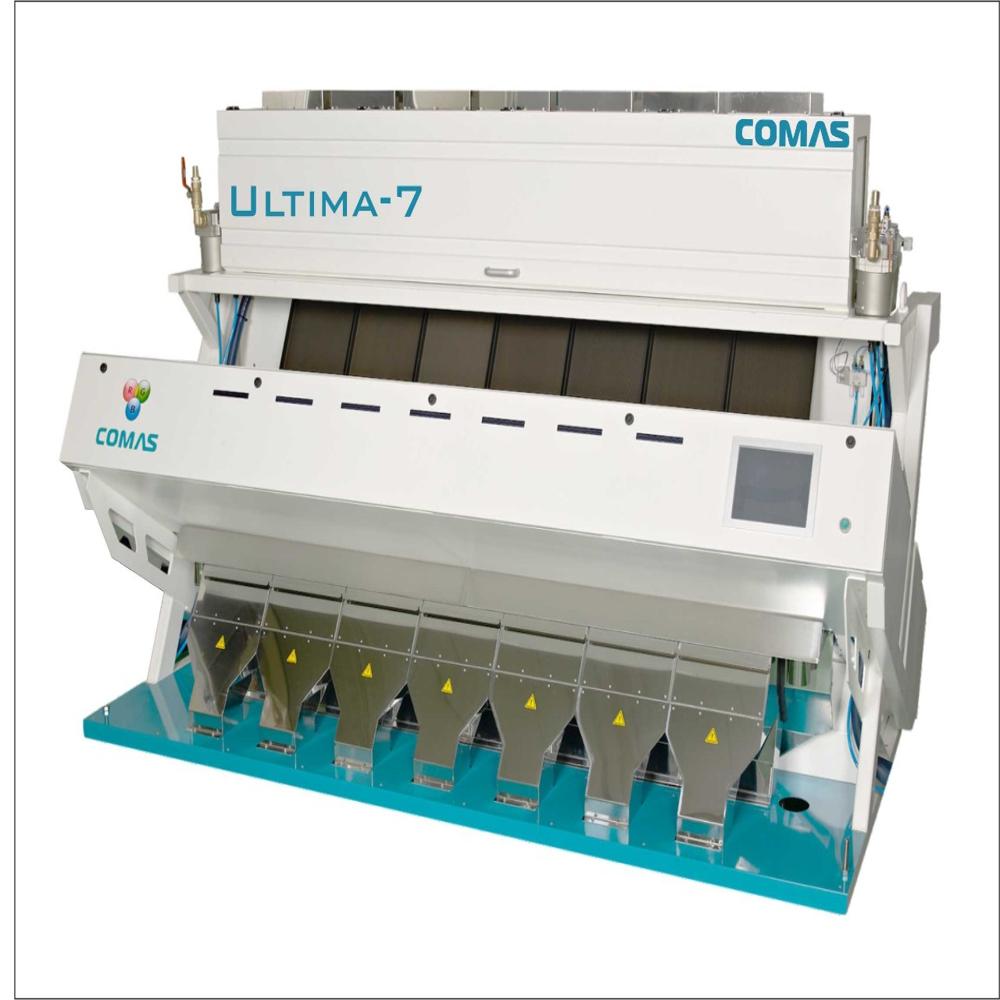
Pulses Color Sorter
Price 500000.0 INR/ Unit
MOQ : 1 Unit
Pulses Color Sorter Specification
- Output
- High Efficiency
- Air Pressure
- 0.8 MPa
- Air Compressor
- 7.5 HP
- Capacity
- 2.5-3.0 Tons/Hour
- Power
- 2.0 KW
- Channels
- 192
- Accuracy
- 98-99%
- Application
- Sorting Pulses Based on Color
- Type
- Pulses Color Sorter
- Dimension (L*W*H)
- 2100 x 1630 x 2040 mm
- Usage
- Industrial
- Weight
- 820 kg
- Feeding System
- Vibratory With Uniform Flow
- Material Of Construction
- Stainless Steel Frame
- Noise Level
- <70 dB
- Ejector Valve Speed
- 1000 times/sec
- Sorting Technology
- CCD Camera and LED-based Optical Sorting
- Power Supply
- 220V/50Hz
- Display
- 7 inch Touchscreen Interface
- Cleaning System
- Automatic Dust Cleaning
- Operating Temperature
- 0C-45C
- Sorting Layers
- Single Layer with Multi-Channel Ejection
- Reject Ratio
- 8:1
Pulses Color Sorter Trade Information
- Minimum Order Quantity
- 1 Unit
- Delivery Time
- 10-15 Days
About Pulses Color Sorter
The RGB Rice Sorter is a semi-automatic sorting machine designed for industrial applications. With multiple channels, this machine is capable of sorting rice based on color, size, and quality. It comes with an air compressor to ensure smooth and efficient operation. The output of this machine is normal, making it suitable for medium to large scale rice processing facilities.
FAQs of RGB Rice Sorter:
Q: What is the application of the RGB Rice Sorter?
A: The RGB Rice Sorter is designed for industrial use.Q: What type of sorting machine is it?
A: It is a semi-automatic sorting machine.Q: Does it have multiple channels?
A: Yes, it comes with multiple channels for sorting.Q: What is the output capacity of the machine?
A: The output of this machine is normal.Q: Does it come with an air compressor?
A: Yes, it comes with an air compressor for efficient operation.Efficient Pulses Sorting Technology
Harnessing CCD camera and LED-based optical sorting, this machine identifies subtle color differences among pulses, delivering high accuracy every cycle. The 192-channel, single-layer ejection process ensures precision and speed, maximizing output efficiency with a throughput of 2.5-3.0 tons per hour. Suited for a broad range of industrial requirements.
User-Friendly Operations and Controls
The 7-inch touchscreen interface allows operators to easily set parameters and monitor performance. With automatic cleaning systems and low noise operation, the machine is engineered for seamless, continuous use in industrial environments.
Durable Build for Industrial Use
Constructed with a robust stainless steel frame, this sorter is designed for durability and hygiene. Its automatic dust cleaning prolongs machine life, while the vibratory feeding system enables uniform flow for consistent sorting quality.
FAQ's of Pulses Color Sorter:
Q: How does the Pulses Color Sorter's sorting process work?
A: The Pulses Color Sorter uses CCD cameras and LED-based optical technology to detect color variations in pulses. It then deploys high-speed ejector valves to remove off-color or defective items, ensuring only quality pulses proceed further.Q: What are the main benefits of using this color sorter in industrial applications?
A: Key benefits include high throughput (up to 3.0 tons/hour), 98-99% sorting accuracy, reduced labor demands due to automation, and superior product uniformity. Its automatic cleaning and robust construction support continuous, low-maintenance operation.Q: Where can the Pulses Color Sorter be effectively applied?
A: This machine is ideal for sorting pulses in food processing plants, agricultural distribution centers, or any industrial facility requiring precise color-based sorting of bulk materials.Q: When should I perform cleaning or maintenance on the sorter?
A: The system features automatic dust cleaning, so routine manual cleaning is minimized. However, periodic checks according to manufacturer guidelines are recommended to ensure continued optimal performance.Q: What is the reject ratio, and why is it important?
A: The reject ratio is 8:1, indicating that for every eight rejected particles, only one good particle may be lost, which demonstrates high sorting precision and minimized product wastage.Q: How is the machine operated and monitored?
A: Operations are managed through a 7-inch touchscreen interface, allowing users to adjust parameters, monitor the sorting process, and review real-time performance data efficiently.Q: What is the usage benefit of the vibratory feeding and multi-channel ejection system?
A: The vibratory feeding system provides a uniform, controlled material flow, enhancing sorting effectiveness. Combined with multi-channel ejection, this ensures high-speed, consistent sorting with minimal blockages.

Tell us about your requirement

Price:
Quantity
Select Unit
- 50
- 100
- 200
- 250
- 500
- 1000+
Additional detail
Mobile number
Email

More Products in Sorter Machine Category

Plastic Color Sorter Machine
Price 500000.0 INR / Unit
Minimum Order Quantity : 1 Unit
Channels : 64
Power : 2.5 kW
Accuracy : 99%
Type : Plastic Color Sorter Machine
Cashew Sorting Machine
Price 500000.0 INR / Unit
Minimum Order Quantity : 1 Unit
Channels : 5
Power : 2.5 kW
Accuracy : 98%
Type : Automatic Cashew Sorting Machine
Grain Color Sorter Machine
Price 500000.0 INR / Unit
Minimum Order Quantity : 1 Unit
Channels : 64 to 256 channels (Modeldependent)
Power : 36 kW
Accuracy : 99%
Type : Grain Color Sorter Machine

Pulses Sorting Machine
Price 500000.0 INR / Unit
Minimum Order Quantity : 1 Unit
Channels : 32 Channels
Power : 3.5 KW
Accuracy : 99%
Type : Pulses Sorting Machine

GST : 36ABICS0252L1Z6
Plot No 63, Hi-tech Theater Ln, Arunodaya
Colony, Sri Sai Nagar, Madhapur,Hyderabad - 500081, Telangana, India
Phone :07971671060
 Send Inquiry
|
 |
SAANVIKA SOFTWARE SOLUTIONS PRIVATE LIMITED
All Rights Reserved.(Terms of Use) Developed and Managed by Infocom Network Private Limited. |
