


 Send Inquiry
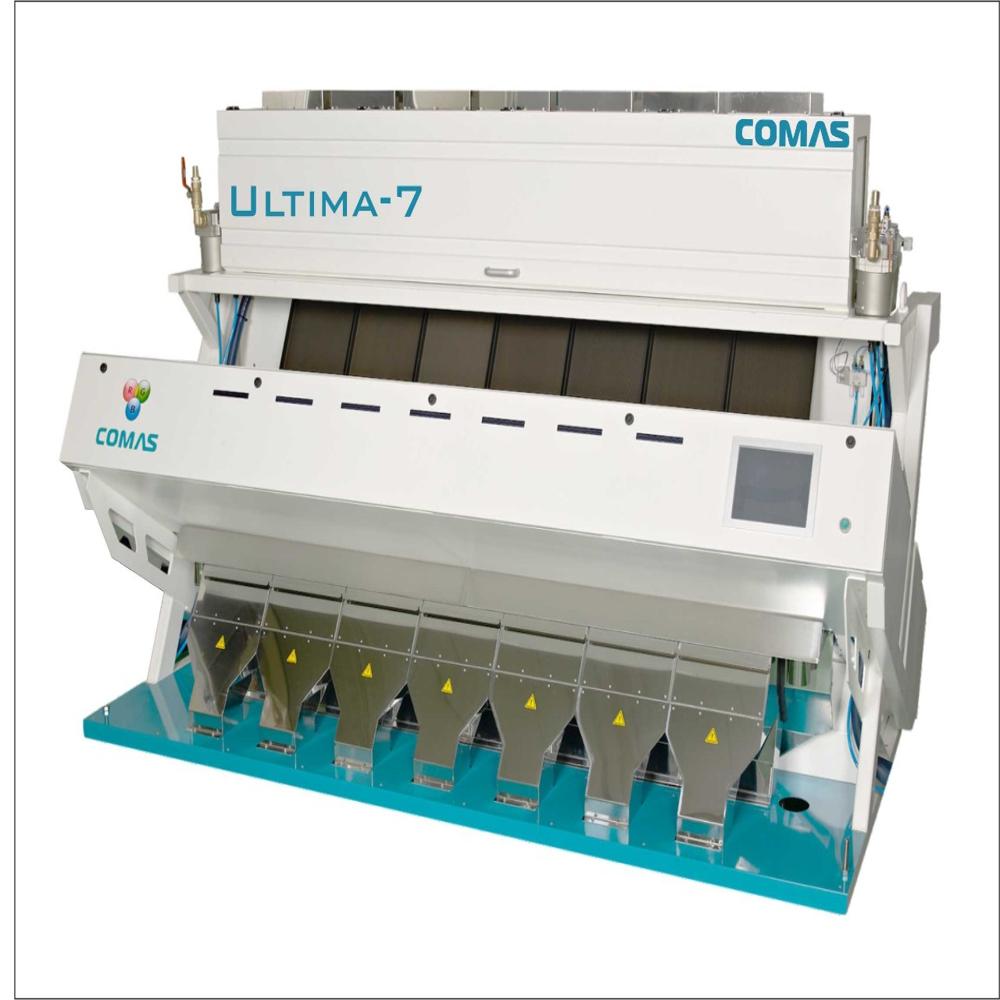
Cereal Color Sorter
Price 500000.0 INR/ Unit
Cereal Color Sorter Specification
- Type
- Cereal Color Sorter
- Air Pressure
- 0.6-0.8 MPa
- Application
- Food Processing Industry
- Capacity
- 2-4 Tons per hour
- Weight
- Approx. 700 kg
- Air Compressor
- 7.5 HP
- Channels
- 6
- Power
- 2.5 kW
- Usage
- Cereal Sorting
- Dimension (L*W*H)
- 1600x1620x1850 mm
- Output
- High Output
- Accuracy
- 99.9%
- Camera Resolution
- 2048 Pixel Full Color CCD
- Sorting Precision
- 99%
- Operation Panel
- Touch Screen
- Ejector
- Electromagnetic Valve
- Voltage
- 220V / 50Hz
- Lighting Source
- LED
- Reject Ratio
- 0.2%
Cereal Color Sorter Trade Information
- Minimum Order Quantity
- 1 Unit
- Delivery Time
- 10-15 Days
About Cereal Color Sorter
FAQs of RGB Rice Sorter:
Q: What is the application of the RGB Rice Sorter?
A: The RGB Rice Sorter is designed for industrial use.Q: What type of sorting machine is it?
A: It is a semi-automatic sorting machine.Q: Does it have multiple channels?
A: Yes, it comes with multiple channels for sorting.Q: What is the output capacity of the machine?
A: The output of this machine is normal.Q: Does it come with an air compressor?
A: Yes, it comes with an air compressor for efficient operation.Advanced Cereal Sorting Technology
Equipped with a high-resolution 2048 pixel full-color CCD camera and LED lighting source, the Cereal Color Sorter ensures precise detection and removal of defective products. Its electromagnetic valve ejectors, combined with advanced air pressure, provide accurate and efficient sorting, tailored for various types of cereals.
User-Friendly Design for Maximum Efficiency
The machine features a modern touch screen operation panel and a high-capacity output of 2-4 tons per hour. Its 6-channel design ensures high throughput and consistent sorting quality, making it a reliable choice for large-scale cereal processors within the food industry in India.
Reliable and Robust Construction
Built to last, the Cereal Color Sorter operates optimally with a 7.5 HP air compressor and consumes just 2.5 kW of power. Its compact design (1600x1620x1850 mm) and approximately 700 kg weight allow for easy installation and integration into existing food processing lines.
FAQ's of Cereal Color Sorter:
Q: How does the Cereal Color Sorter achieve such high sorting precision?
A: The sorter uses cutting-edge 2048 pixel full-color CCD cameras and precise LED lighting, allowing for accurate detection of color defects. Coupled with fast electromagnetic valve ejectors, it achieves up to 99% sorting precision and 99.9% accuracy, ensuring consistent results.Q: What types of cereals can be processed with this color sorter?
A: This machine is designed to handle a wide variety of cereals, including rice, wheat, barley, lentils, and other grains, making it suitable for diverse applications in the food processing industry.Q: When is it beneficial to use a color sorter in cereal processing?
A: A color sorter becomes especially valuable when high sorting accuracy and capacity are required, such as in large-scale food processing plants aiming to maintain stringent quality standards and improve product value.Q: Where can the Cereal Color Sorter be installed and operated?
A: The machine is suitable for use in factories, mills, or processing plants across India, as it operates on standard 220V/50Hz power, and its dimensions allow for integration into most cereal sorting lines.Q: What is the sorting process followed by this machine?
A: Cereals are fed into the sorter, where they are inspected by the CCD camera system under LED lighting. Defective or discolored grains are identified and swiftly removed by targeted air ejectors, ensuring only high-quality product exits the system.Q: What are the main benefits of using this cereal color sorter?
A: The key advantages include high output (2-4 tons/hour), exceptional sorting precision, minimal product rejection (0.2% reject ratio), and labor cost savings. It enhances overall product quality and protects brand reputation.Q: How easy is the machine to operate and maintain?
A: With its intuitive touch screen interface and robust engineering, the color sorter is straightforward to operate. Regular maintenance is simplified due to accessed panels and reliable components supplied by trusted distributors and suppliers in India.


Price:
- 50
- 100
- 200
- 250
- 500
- 1000+

More Products in Sorter Machine Category

Color Sorter
Price 50000.0 INR / Unit
Minimum Order Quantity : 1 Unit
Dimension (L*W*H) : 1620 x 1530 x 1840 mm
Output : Variable, depends on material
Accuracy : >99%
Usage : Sorting granular materials by color

Wheat Sorting Machine
Price 500000.0 INR / Unit
Minimum Order Quantity : 1 Unit
Dimension (L*W*H) : 2100 1590 1895 mm
Output : Customizable
Accuracy : 99%
Usage : Grain Sorting

Plastic Color Sorter Machine
Price 500000.0 INR / Unit
Minimum Order Quantity : 1 Unit
Dimension (L*W*H) : 1650 mm x 1630 mm x 2000 mm
Output : 450 480 kg/h
Accuracy : 99%
Usage : Sorting of plastic granules and flakes
Grain Color Sorter Machine
Price 500000.0 INR / Unit
Minimum Order Quantity : 1 Unit
Dimension (L*W*H) : 2200 x 1550 x 2100 mm (Varies by model)
Output : Selectable, up to 5 tons/hour
Accuracy : 99%
Usage : Grain Sorting

GST : 36ABICS0252L1Z6
 Send Inquiry
|
 |
SAANVIKA SOFTWARE SOLUTIONS PRIVATE LIMITED
All Rights Reserved.(Terms of Use) Developed and Managed by Infocom Network Private Limited. |
